Refrigerator Manufacturing Plant Cost & Turnkey Line

Production line for

Refrigerator Manufacturing Plant Cost & Turnkey Production Line

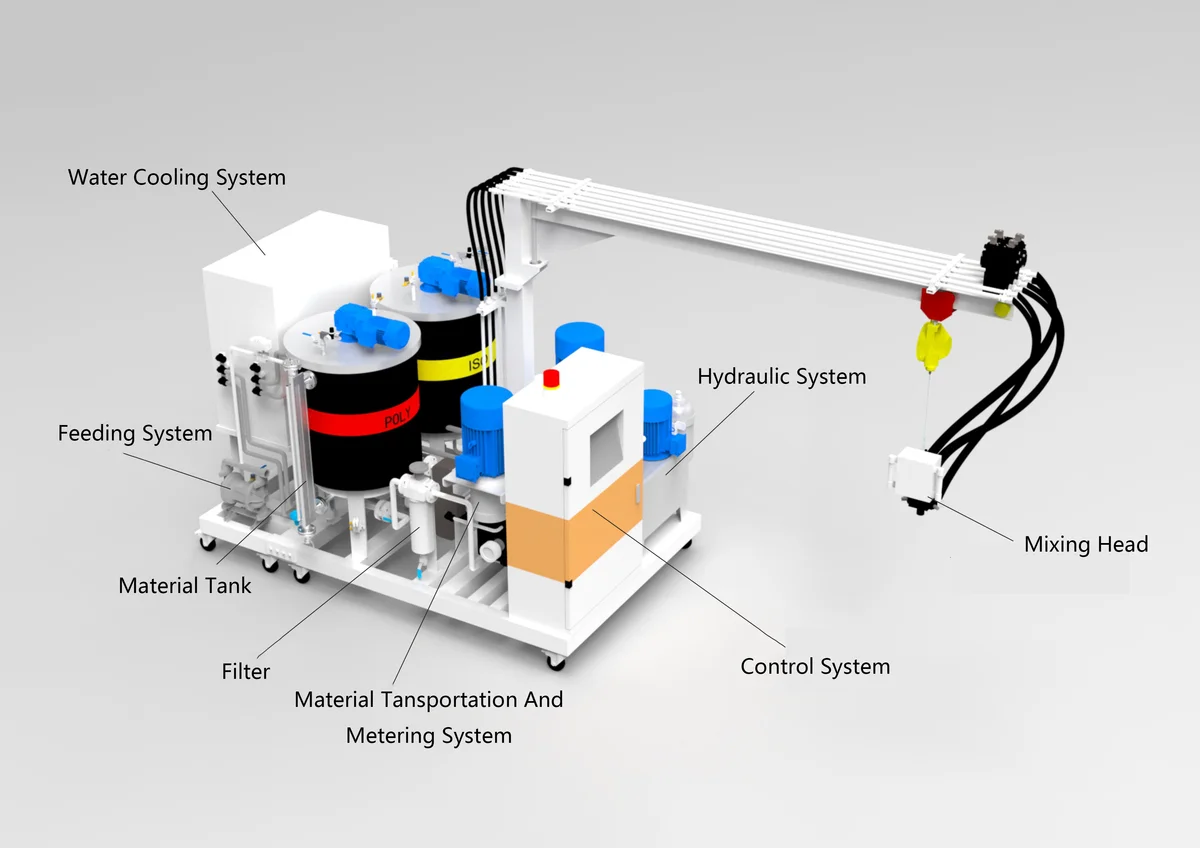
We engineer and supply turnkey refrigerator cabinet foaming lines — vacuum-forming moulds, high-pressure PU foaming machines, ground-rail assembly — with 500 to 2,450 doors/shift of door-foaming capacity on the ground-rail line.

$

Investment Range

USD 800K – 5M · 500 to 2,450 doors/shift is door-foaming capacity; finished-refrigerator output is sized separately

Who Buys This Line

Household & commercial refrigerator OEMs building or expanding a plant

Certification Ready

IEC 60335-2-24 · EN 62552 · DOE · CE · RoHS ready

In one line

200+ refrigerator designs in our reference library — use them as-is, or we customize to your bill of materials.

If you're a refrigeration cabinet manufacturer planning a new production line or expanding existing capacity, UREXCEED supplies the vacuum-formed door moulds, high-pressure PU foaming machines and ground-rail assembly systems as one turnkey line — with 500 to 2,450 doors/shift of door-foaming capacity and IEC/EN/DOE/CE-ready configuration.

01

Built for refrigeration cabinet manufacturers

For household and commercial refrigerator manufacturers opening a new plant or expanding an existing one. Configurations scale from a single-station entry line to a 26-station ground-rail system.

Door-foaming output
500–2,450 doors/shift on the ground-rail line (single-cavity, 20s takt)
02

One integrated production stack

Cabinet and door moulds, high-pressure PU foaming, assembly and handling are engineered as one line instead of separate equipment packages.

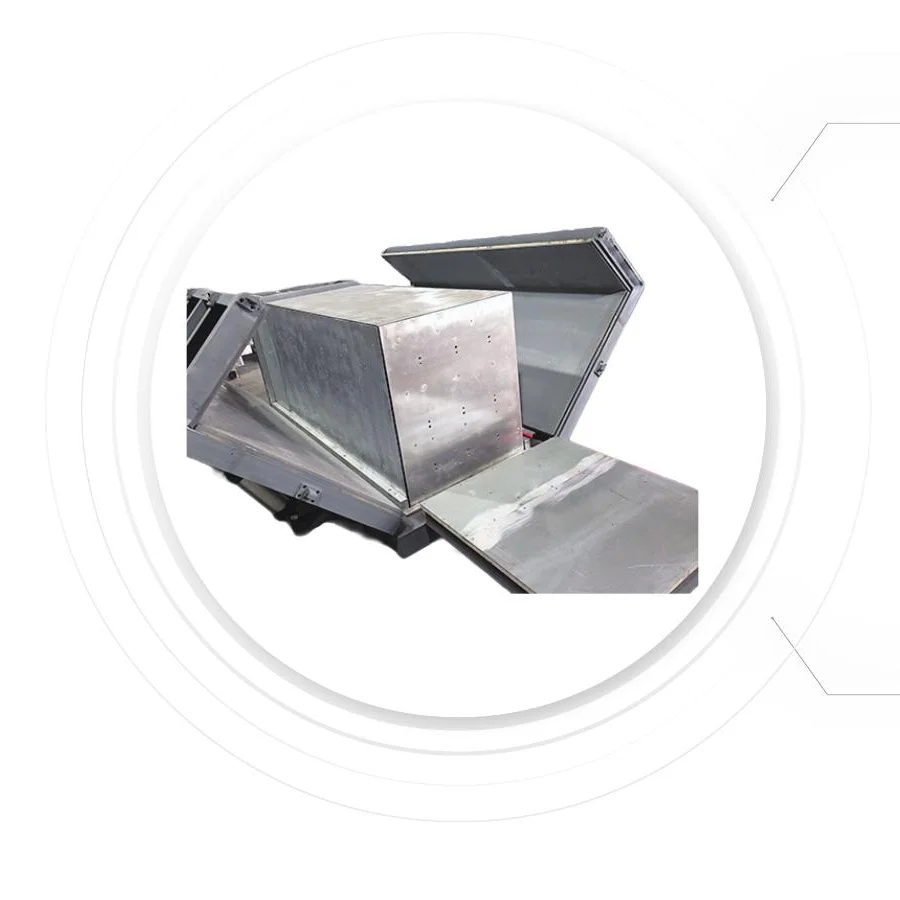
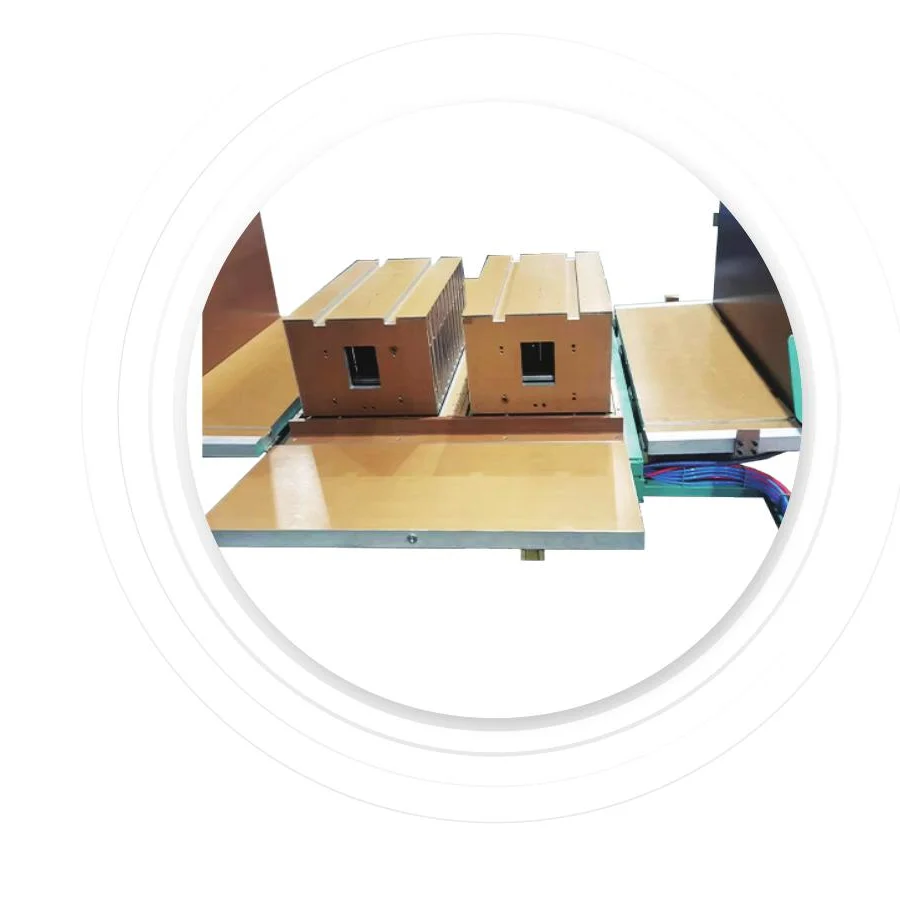
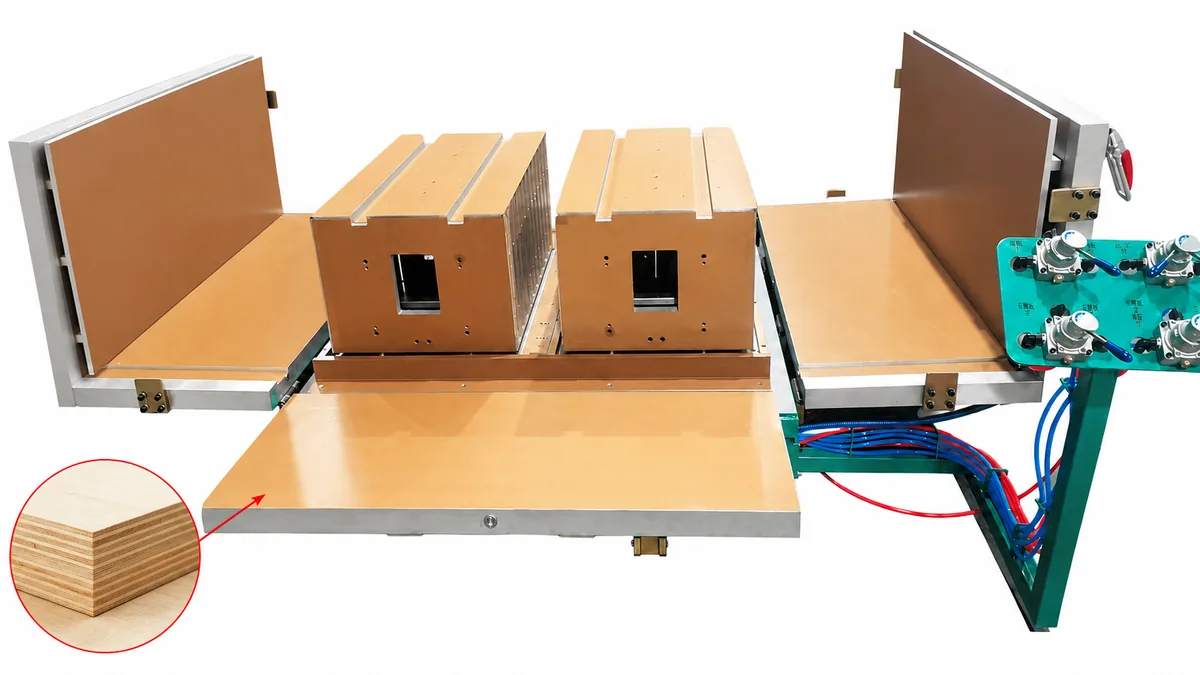
  • ABS/HIPS liner vacuum-forming moulds
  • Cabinet and door foaming moulds
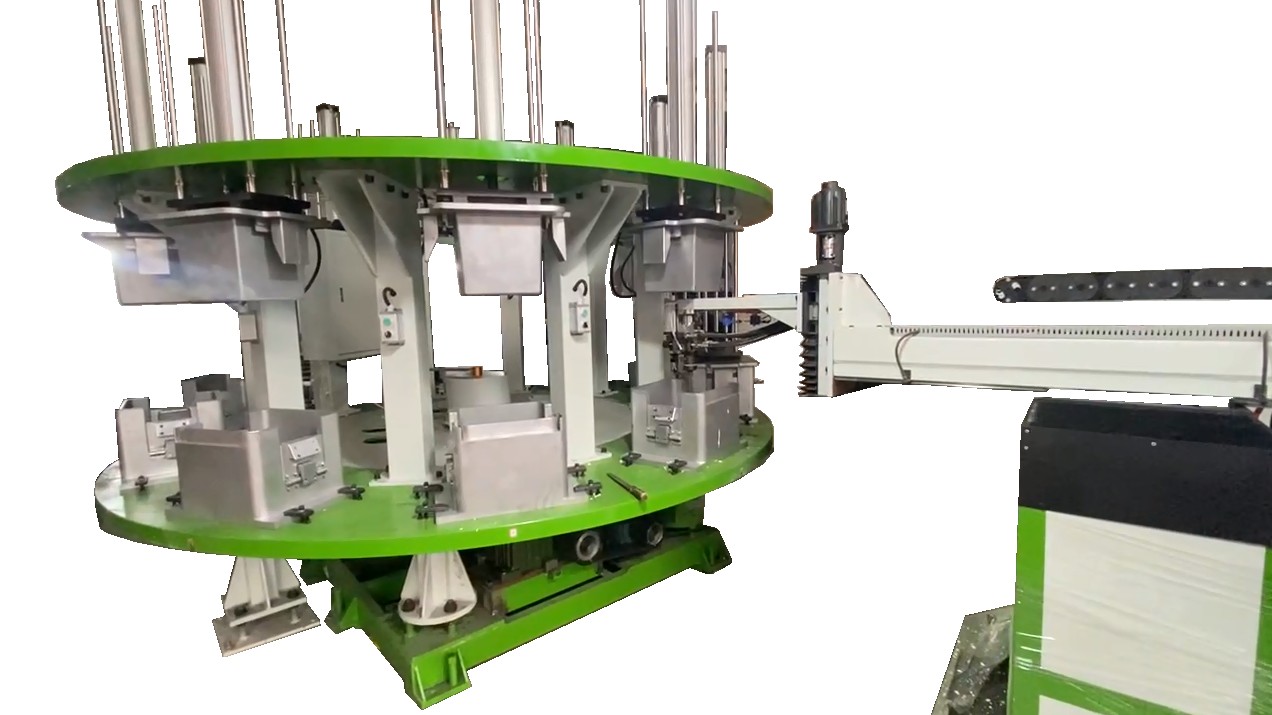
  • Ground-rail or rotary assembly
  • Leak test, foam QA and packaging
03

Cabinet range

Volume
90–700 L; commercial up to 1,200 L
Temperature
+2 to −25 °C; freezer option to −40 °C
Insulation
40–80 mm wall · 32–42 kg/m³ foam
Thermal target
0.020–0.024 W/m·K
04

Compliance-ready configuration

Equipment and reference cabinet specifications can be configured around IEC 60335-2-24, EN 62552, DOE, CE and RoHS requirements.

Cyclopentane projects include ATEX-rated equipment and gas detection. Certification of the finished refrigerator remains with the OEM.

How Much Does a Refrigerator Manufacturing Plant Cost?

Our current equipment data puts refrigerator manufacturing plant cost from USD 800K for a 500-finished-refrigerators/day entry line, USD 1.9M–3.2M for a standard 2,000-finished-refrigerators/day line, and up to USD 5M for a highly automated project. These are equipment and line-integration budgets, not a turnkey building price: land, the factory shell and the country-specific costs listed below are outside the equipment quote.

Plant size Finished refrigerators per day Equipment CAPEX Included Not included
Entry plant 500 From USD 800K Core forming, foaming and assembly equipment sized to the confirmed SKU plan Land, building, local charges, inventory and working capital
Standard plant 2,000 USD 1.9M–3.2M Moulds, forming, foaming, conveyor integration, testing, packing, utilities, installation and training Land, building, local charges, inventory and working capital
Highly automated project Project-specific Up to USD 5M Automation, stations and testing configured to the approved project scope Land, building and country-specific owner costs; requote by SKU count, automation and local infrastructure

What the quoted plant cost includes

For the standard 2,000-finished-refrigerators/day case, the quoted USD 1.9M–3.2M budget is built from the following scope:

  • Moulds: USD 350K–550K
  • Vacuum-forming machines: USD 200K–350K
  • High-pressure PU foaming: USD 180K–280K
  • Conveyor and integration: USD 400K–700K
  • Testing equipment: USD 250K–400K
  • Packing line: USD 150K–250K
  • Utilities: USD 300K–500K for compressed air, chilled water and electrical distribution
  • Installation and training: USD 100K–200K, including FAT/SAT

The line-item arithmetic is USD 1.93M–3.23M; the published USD 1.9M–3.2M range is the same budget rounded to one decimal place.

Costs not included in the equipment quote

  • Land or lease: varies by country and city; estimate after the project location is confirmed.
  • Factory building and civil works: varies by country, city, soil and site condition; estimate after the project location is confirmed.
  • Local permits and certification: varies by destination market and product class; estimate after the project location is confirmed.
  • Import duty, VAT and inland freight: varies by country, port and city; estimate after the project location is confirmed.
  • Initial raw-material inventory and working capital: varies by SKU mix, supplier terms and local logistics; estimate after the project location is confirmed.
  • Local labour recruitment: varies by city, shift pattern and skill availability; estimate after the project location is confirmed.

What changes the final refrigerator plant cost?

Finished-refrigerator output. Higher daily capacity adds parallel fixtures, conveyor stations, forming capacity and testing throughput.

SKU and mould-change count. More cabinet and door formats add mould sets, quick-change hardware, recipes and commissioning work.

Automation tier. Robots, automatic demoulding, tracking and auto-reject systems increase controls, handling and integration CAPEX.

Cyclopentane ATEX safety. Explosion-rated electrics, gas detection, ventilation and nitrogen blanketing increase the foaming and utility package.

Target-market testing and certification. DOE, IEC/EN, CE or market-specific acceptance targets change the test stations and documentation supplied with the line; finished-appliance certification remains the OEM's responsibility.

Inputs required for a project quotation

Send the site country and city, available floor plan, refrigerator SKU drawings, finished units/day, shifts, automation target, destination-market standards and any equipment already installed.

Request a scoped plant quote →
Real Pains We Hear from Buyers — and What We Ship to Solve Each One

Four pains that almost every refrigerator factory founder brings us in the first call. Here's what we ship to solve each one.

Pain 1

Cabinet wall thickness varies cabinet-to-cabinet — k-factor drifts and the EU energy class type-test fails

How we solve it

Our cast-aluminium foaming moulds hold ±0.05 mm cavity precision across 1,000,000+ cycles, paired with a refrigerator mold fixture that clamps at ±0.5 mm parallelism. PU metering at ±0.5% shot accuracy on UPM-HP-1500. Wall thickness variance drops from ±2 mm to ±0.3 mm — type-test passes first try.

Pain 2

Buying mould + PU machine + fixture + production line from 4 different suppliers — nobody owns the foam quality result

How we solve it

We supply mould + fixture + PU machine + raw materials as one calibrated system. When foam quality drifts, you call one supplier, not four. We can't blame the chemicals if there's a mould issue, and vice versa. One PO, one project manager, one set of acceptance criteria.

Pain 3

EU F-gas regulations from 2025 forced us off HFC — switching to cyclopentane needs ATEX-rated equipment we don't have

How we solve it

Our high-pressure machine is cyclopentane-ready out of the box: ATEX Zone 1 electrics, LEL gas detection at 4 points, N₂ blanket on the day tank, auto-shutdown at 50% LEL. We supply the full EU ATEX certificate pack with the equipment so your local fire authority approves in 2–4 weeks instead of 3–6 months.

Pain 4

First refrigerator factory — we don't know how to design the cabinet, how the foam should cure, how to set up QC

How we solve it

For first-time refrigerator factories, we co-design the cabinet using one of 200+ proven templates in our library — that's a 45-day mould instead of a custom 80-day mould. Our engineers spend 10–15 days on-site for commissioning, run the first 100 cabinets together with your operators, and hand over a foam parameter card that your team can follow without R&D.

What You Need

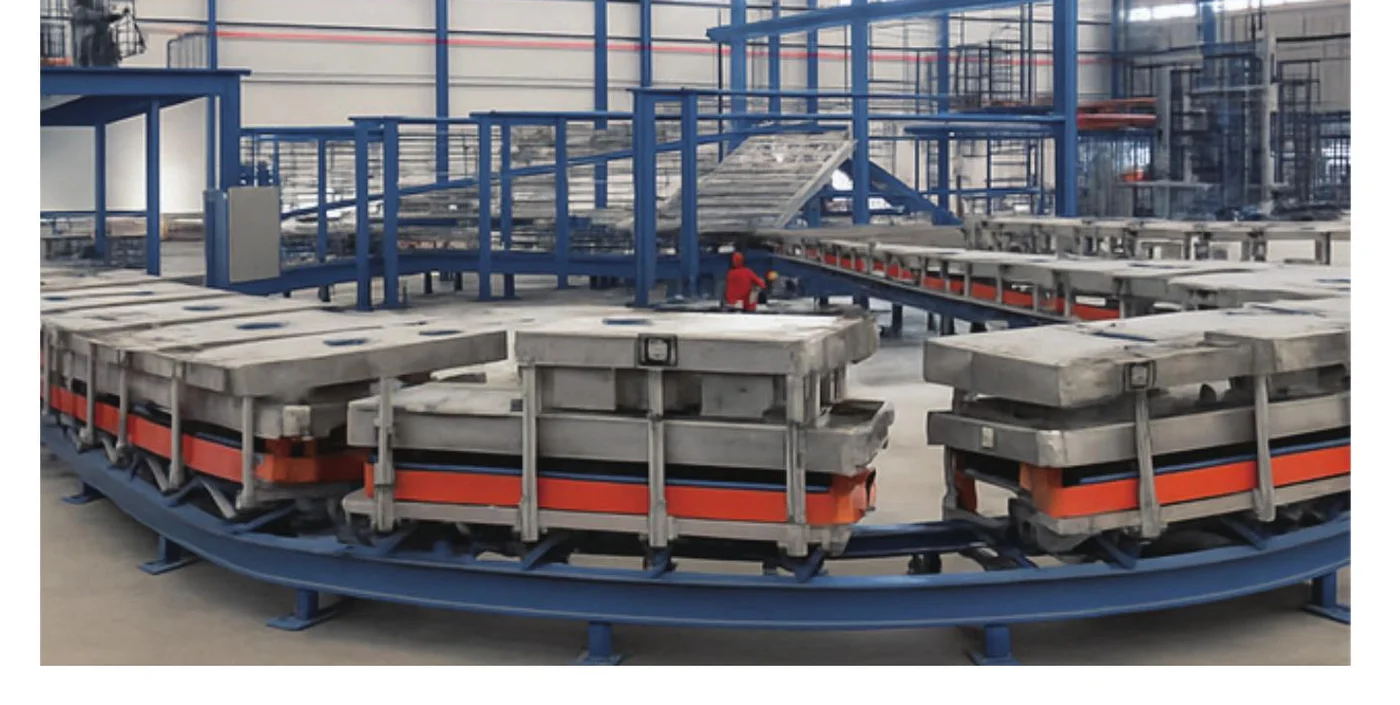
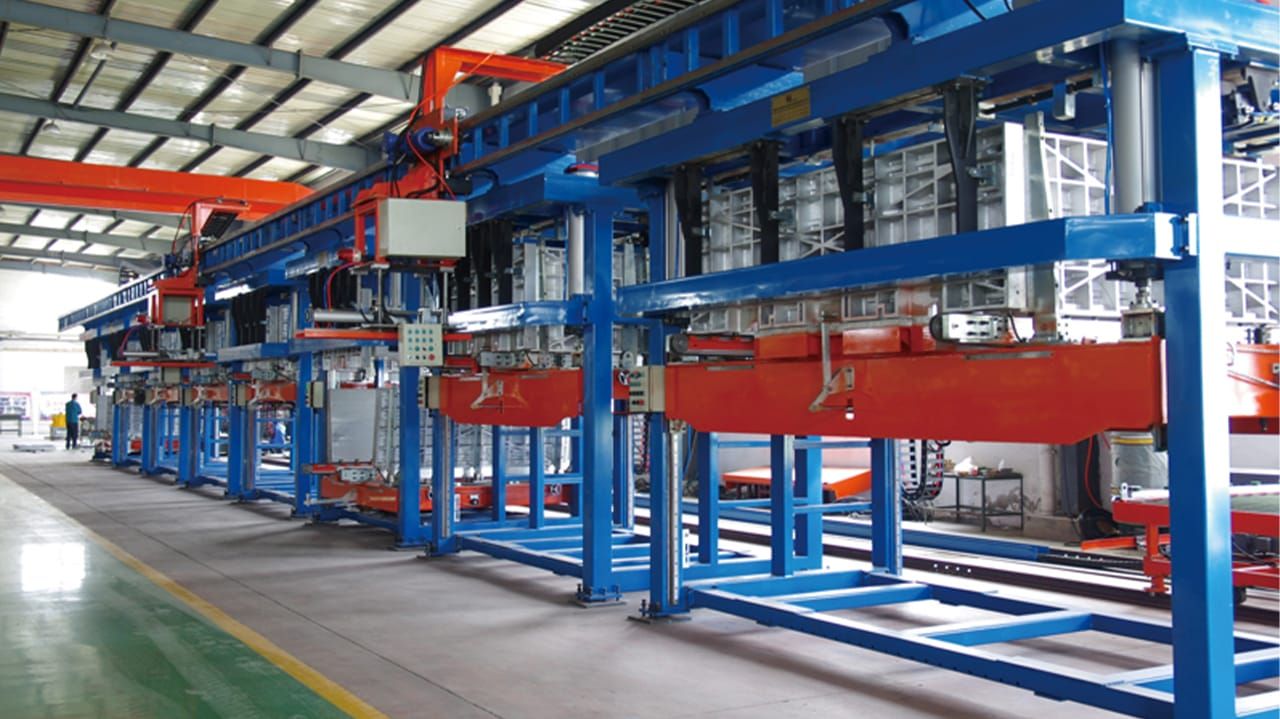
26-Station Ground-Rail PU Foaming Line for Refrigerator Doors — Closed-Loop Track Layout
Production Lines

26-Station Ground-Rail PU Foaming Line for Refrigerator Doors — Closed-Loop Track Layout

Closed-loop ground-rail PU foaming line dedicated to refrigerator and cabinet DOOR foaming. 26 single-cavity fixture stations on a continuous steel track, 20-sec takt, ~1,200 doors per 8-hour shift (~2,450/day on two shifts) at 85% line efficiency. 2,000 × 900 mm fixture × 200 mm closing height — sized for door panels. Cyclopentane + ATEX Zone 1, steam or oil heating.

Learn More
Hardware & Accessories — Bundled with Main Equipment Orders
Hardware & Accessories

Hardware & Accessories — Bundled with Main Equipment Orders

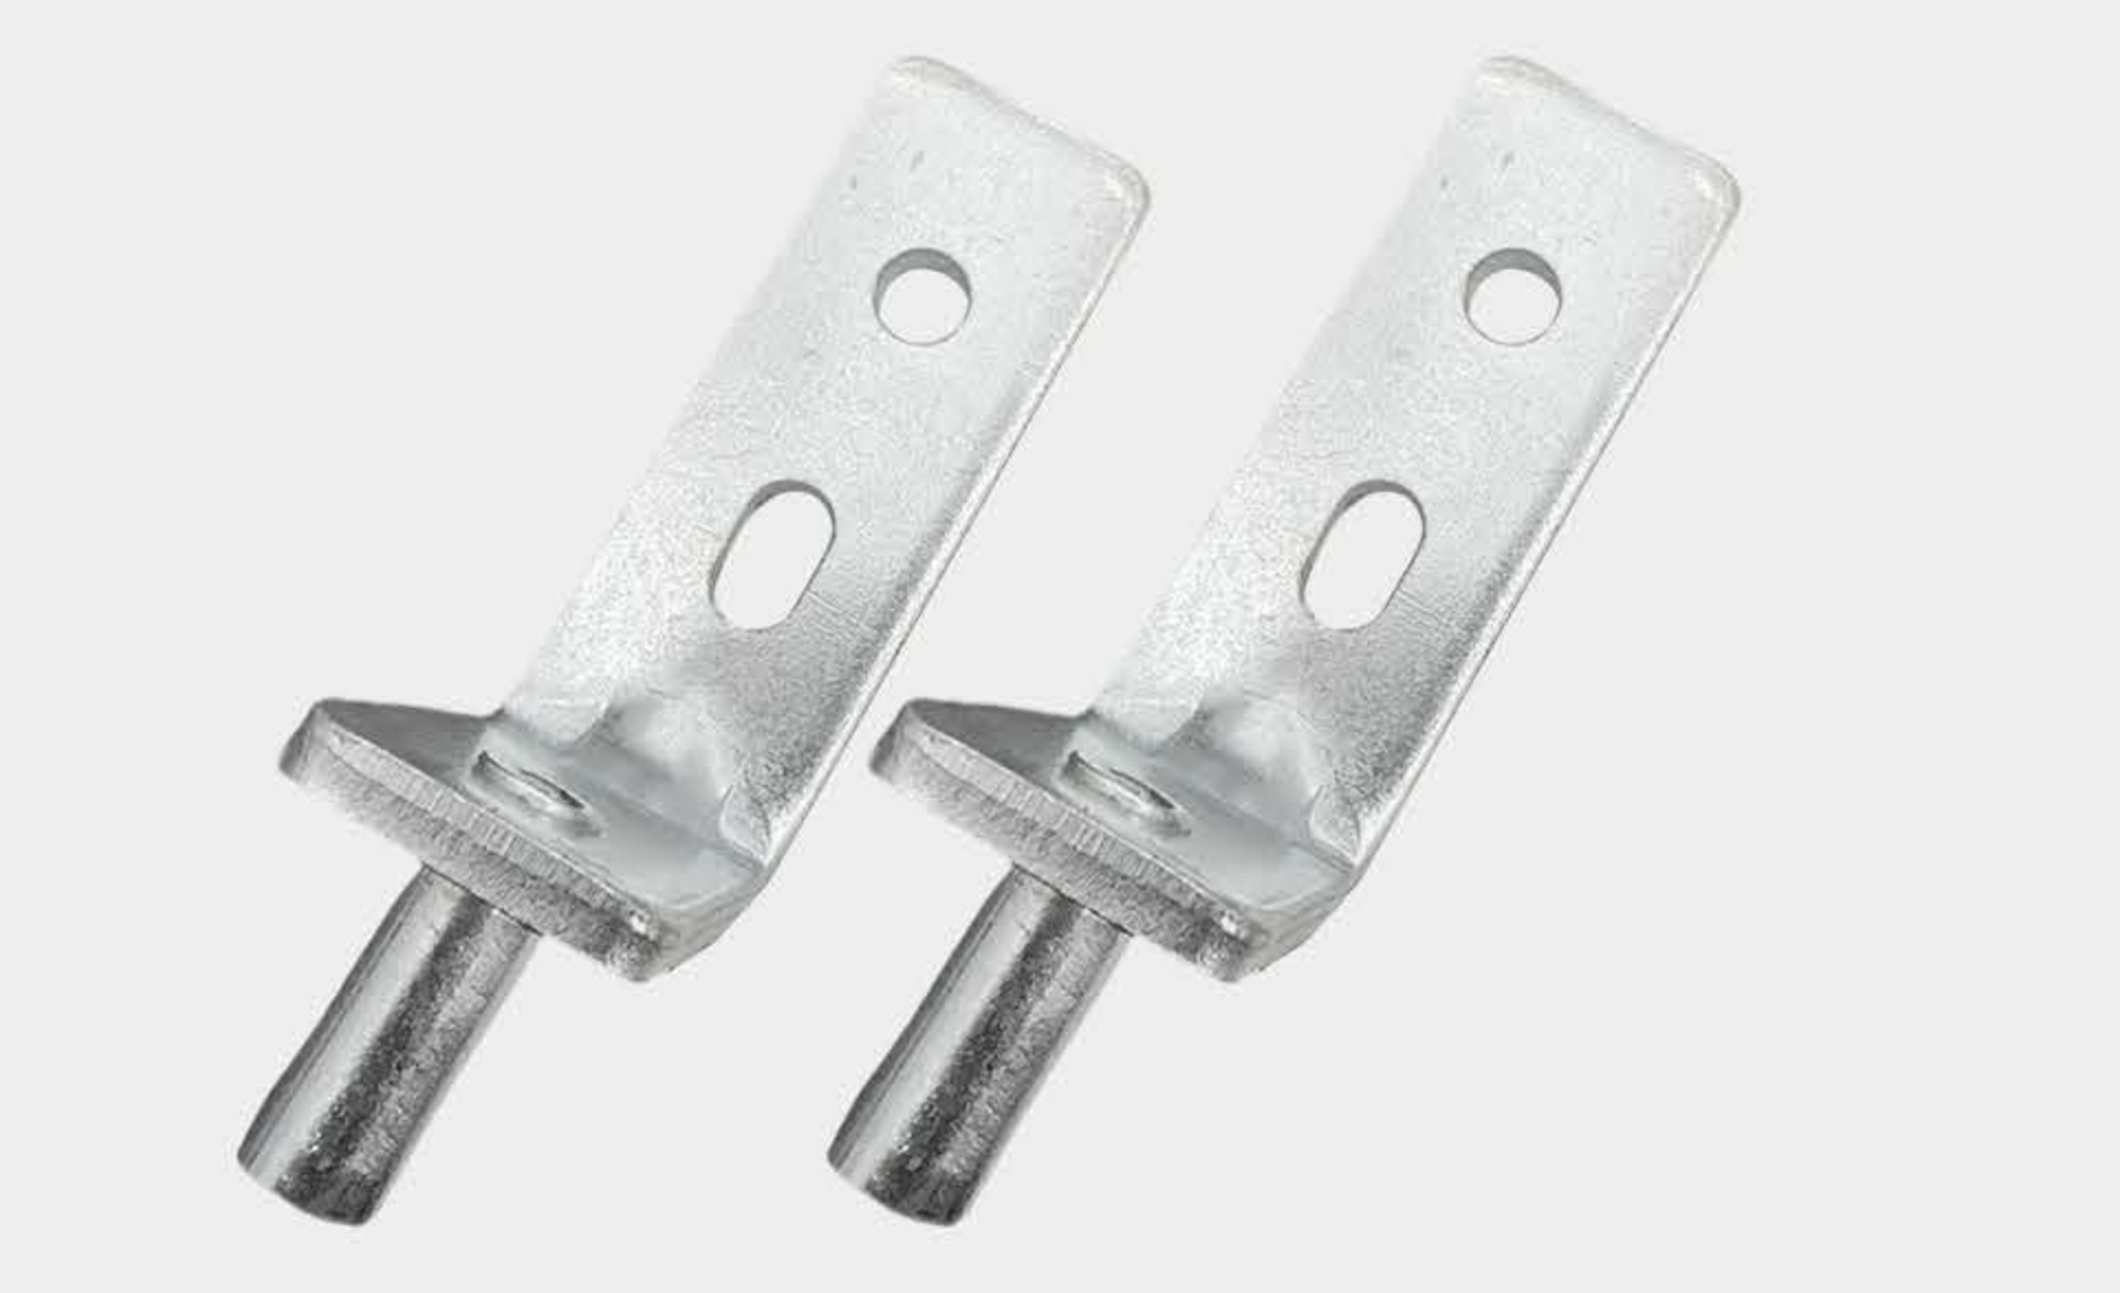
Complementary hardware fabrication service — supplied alongside our main equipment orders (moulds / PU foaming / production line). Custom-fabricated per your drawings: 5 categories — hinges, brackets, rails & ladders, wire shelves & baskets, grid panels. Not a standalone product line. Consolidated into your main shipment.

Learn More
Cyclopentane High-Pressure PU Foaming Machine
PU Foaming Machines

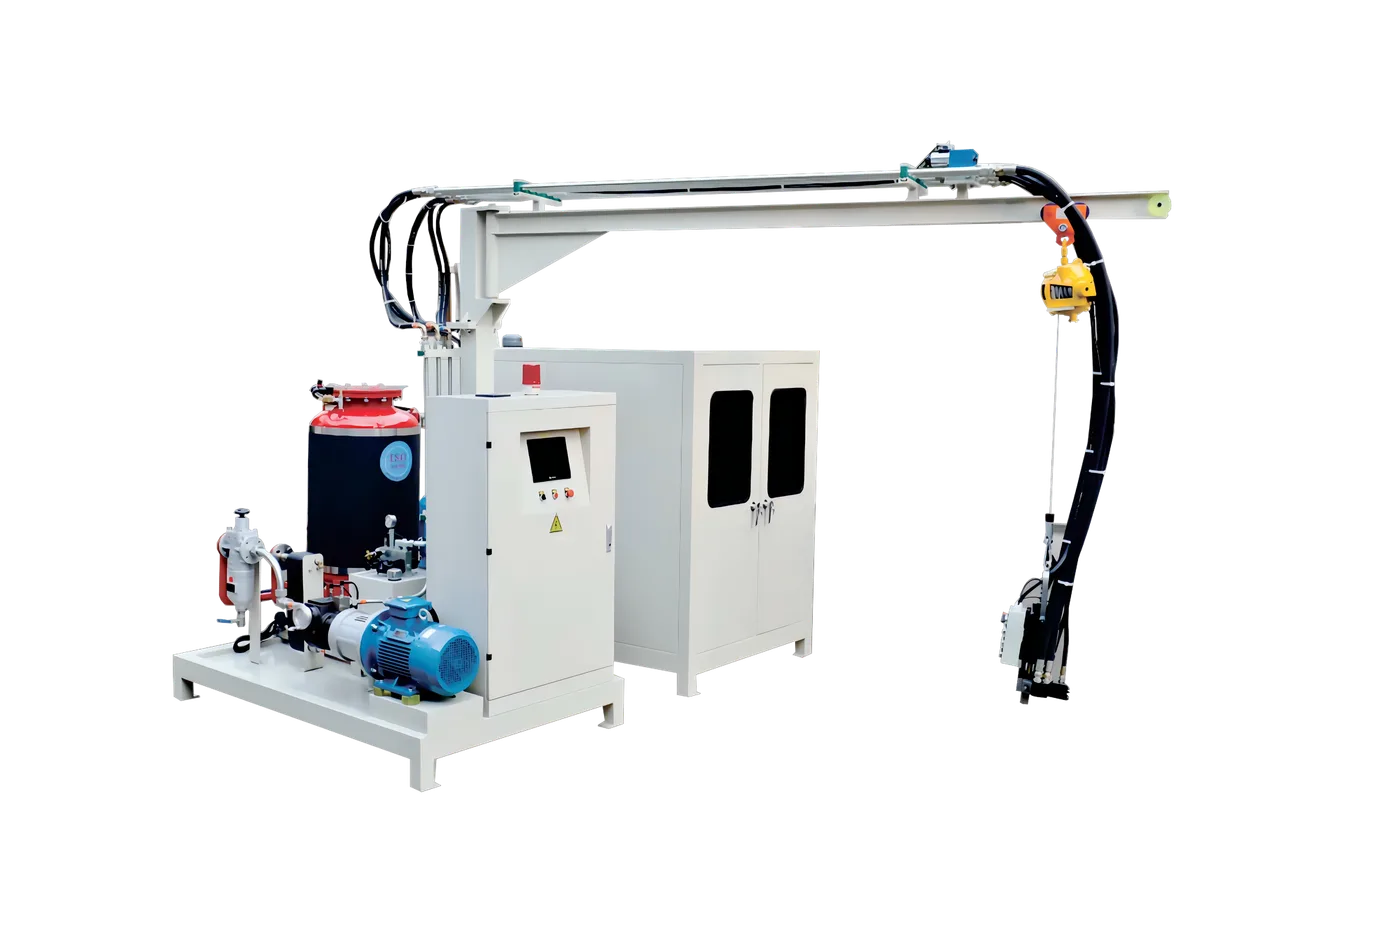
Cyclopentane High-Pressure PU Foaming Machine

Our flagship — purpose-built for refrigerator factories chasing the top EU energy classes (B–C on the 2021 A–G label, formerly A+++). Cyclopentane-ready out of the box with full ATEX Zone 1 safety package. Three sizes covering 500 to 8,000 cabinets a day.

Learn More
Mold for Horizontal Freezer (Chest Freezer Cabinet)
Refrigerator Mould (Mold) — Vacuum-Forming, Foaming, Door & Liner Moulds

Mold for Horizontal Freezer (Chest Freezer Cabinet)

Refrigerator / freezer mould (mold) for chest freezers — cast aluminium ZL105 / LY12 PU foaming mould. Single-temperature single-top, single-temperature double-top, and dual-temperature double-top variants. Up to 1,500 × 700 × 900 mm cabinet, 6–10 min curing.

Learn More
Mold for Upright Kitchen Refrigerator
Refrigerator Mould (Mold) — Vacuum-Forming, Foaming, Door & Liner Moulds

Mold for Upright Kitchen Refrigerator

Refrigerator mould (mold) for upright kitchen refrigerator cabinets — cast aluminium PU foaming mould for commercial 2-door / 4-door / 6-door upright stainless kitchen refrigerators. Up to 1,900 × 900 × 2,000 mm. Designed for energy-efficient deep cavities and long mould life.

Learn More
PU Raw Materials System
PU Raw Materials

PU Raw Materials System

We make refrigerator-grade PU systems — polyol blend, MDI, blowing agent, all formulated in our own plant. k-factor down to 0.018, density customizable, tuned to your cabinet and your line.

Learn More

Cabinet models you can produce on this line

Every row below is a real cabinet SKU that customers already produce using the moulds in this line — temperature class, capacity, compressor, refrigerant and overall dimensions are field-tested. Use the matrix to match your target cabinet to the right mould configuration.

Cabinet model Variant Temperature (°C) Volume (L) Power (W) Weight (kg) Compressor Refrigerant Size (mm) Source mould
CFD-40D2F-K 2-door freezing -23 to -18 900 740 150 DONPER / WANBAO R290 1210 × 805 × 1950 Mold for Upright →
CFD-60D3F-K 3-door freezing -23 to -18 1395 1033 200 DONPER / WANBAO R290 1820 × 805 × 1950 Mold for Upright →
CFR-40D4F (HB) Air-cooled refrigeration · Engineering Version -2 to 10 925 330 115 DONPER / WANBAO R290 1210 × 805 × 1950 Mold for Upright →
CFR-60D6F (HB) Air-cooled refrigeration · Engineering Version -2 to 10 1430 500 155 DONPER / WANBAO R290 1820 × 805 × 1950 Mold for Upright →
CFS-40N4HF (HB) Dual-temp air-cooled · Engineering 0–10 | ≤-21 782 586 116 DONPER / WANBAO R290 1210 × 805 × 1950 Mold for Upright →
CFS-60N6HF (HB) Dual-temp air-cooled · Engineering 0–10 | ≤-21 1215 1015 156 DONPER / WANBAO R290 1820 × 805 × 1950 Mold for Upright →
BC/BD-268 — 0–10 or ≤-18 268 110 59 DONPER / WANBAO R600a 955 × 635 × 845 Mold for Horizontal →
BC/BD-358 — 0–10 or ≤-18 358 118 65 DONPER / WANBAO R600a 1110 × 635 × 845 Mold for Horizontal →

Source: UREXCEED catalog §07 OEM/ODM cabinet series, cross-referenced to the mould that produces each SKU. Custom cabinet sizes outside this range supported — send us your cabinet drawing for a 7-day quote.

From inquiry to first commercial unit — the 6-step delivery flow

From your first inquiry to the first commercial refrigerator rolling off your line. ~12 months total for a standard line producing 2,000 finished refrigerators/day.

Refrigerator Manufacturing Plant Cost & Turnkey Line — production line reference
  1. 1

    Inquiry & Site Survey

    Week 1–2

    You share target capacity, cabinet size mix, target export markets, factory location. We send a 1-page proposal with line layout and price range. Optional remote site survey (video + drone footage) or in-person visit (USD 1.5K survey fee, refundable against order).

  2. 2

    Detailed Proposal & Pricing

    Week 2–4

    Our engineering team designs the foaming line layout for your factory, picks mould models from our 200+ template library, sizes the PU machine, drafts the BOM. Final quote with 20-line breakdown delivered in 14 days. 2–3 quote revisions typical.

  3. 3

    Contract & Cabinet Design Freeze

    Week 4–8

    Contract signed with 30% down payment. Cabinet CAD review — you send your final cabinet drawings (DWG/STEP), our engineers convert to mould design, you approve the mould CAD before machining starts.

  4. 4

    Manufacturing & In-House QC

    Month 3–7

    Moulds: 45–80 days CNC + heat treatment + polishing. PU machine: 45–60 days in parallel. Line conveyor + fixtures: 60–90 days. Each item tested in our QC lab before shipping. You get monthly progress reports + video walkthroughs.

  5. 5

    Sea Freight & On-Site Installation

    Month 7–10

    6–8 × 40' containers ship from Shanghai/Ningbo. Customs clearance handled by you. On-site installation by our 5–8-person engineer team, 3–4 weeks (foundation, electrical, water/steam, line assembly).

  6. 6

    Commissioning, Training & Acceptance

    Month 10–12

    First 100 trial cabinets foamed together with your operators. Foam parameter card hand-over. 5-day operator training. Acceptance signed when 50 consecutive cabinets pass k-factor + dimensional spec. 60% payment due here, remaining 10% after 3-month performance verification.

Refrigerator platform engineering

Cabinet Platform & Line Configuration

Every refrigerator line we ship is customized on 4 axes. The line stays modular — change one axis without re-tooling the others.

Cabinet size & form

120 L – 800 L: top-mount, bottom-mount, French-door, side-by-side, built-in. Mould design adapts within our 200+ template library.

Voltage / Frequency / PLC

110V / 220V / 380V × 50/60Hz combinations. Siemens / Mitsubishi / Delta PLC choices. Pre-wired for your target market.

Cosmetic finish & branding

Cabinet RAL color, door handle / hinge brands (Sugatsune / Hettich), Osram LED interior, your brand decals factory-fitted.

Automation tier

500 finished refrigerators/day pilot → 10,000 finished refrigerators/day full-scale on the same modular backbone. ABB / KUKA robot integration optional.

Shared engineering reference

PU foam quality, testing and acceptance

Closed-cell ratio, density uniformity and thermal testing are documented once in our quality center.

View quality standards →

Questions factory owners ask us

How long does it take to commission a new refrigerator line?
Mould design and production: 45–75 days. Foaming machines: 45–60 days in parallel. Line integration: 120–180 days. Shipping and commissioning: 60–90 days. Total from signed contract to first commercial unit: 8–12 months for a standard line, 14–18 months with site-specific customization.
What is the typical investment for a line producing 2,000 finished refrigerators/day?
USD 1.9M–3.2M for a standard line producing 2,000 finished refrigerators/day. This equipment and integration budget includes moulds, forming, foaming, conveyor integration, testing, packing, utilities, installation and training. Land, the factory building, local permits and taxes, inland freight, initial inventory, working capital and local recruitment are not included.
Can you customize cabinet size, voltages and branding?
Yes. All moulds support custom cabinet dimensions (from 120 L up to 500 L+ on single line). Foaming machines support 110V / 220V / 380V, 50Hz / 60Hz, Siemens / Mitsubishi / Delta PLC brands. Door hardware, seals, hinges and LED lighting ship in client-specified colours and branding.
What certifications do the equipment carry — and what do I still need to obtain?
Our equipment ships with CE + ISO 9001 certification. Appliance-level certifications (UL, ETL, EAC, CB, energy labels) are obtained by you the factory on finished refrigerator units — we supply testing infrastructure (pull-down, leak, electrical safety) to make that process routine.
How much factory area does a line producing 2,000 finished refrigerators/day need?
6,000 – 7,500 m² for the production floor plus 4,000 m² for raw-material storage and finished-goods logistics. Line length 180–220 m. Single-story reinforced-floor layout recommended — foaming stations require reinforced foundations for the clamping forces.

ROI · Cost Analysis

Refrigerator Plant ROI Example

Use your operating assumptions to calculate project payback; equipment CAPEX alone cannot determine ROI.

Investment
USD 800K – 5M
Payback
Calculate from project inputs
Annual Throughput
60K–300K units/year

Configuration note: Model payback from capacity utilization, annual working days, contribution margin per finished refrigerator, and whether land and the factory building are included. We do not publish a fixed payback period without those four project inputs.

Service & Support

Warranty & Service

On-site intervention available in every region where we have delivered projects.

On-Site Installation

Our engineers fly to your factory to supervise installation, layout verification, and first-run production.

Commissioning + Tuning

Trial run + parameter tuning to your local raw material, climate, and target product spec — until throughput meets contract.

Operator Training

5-10 day on-site training for production team, QC, and maintenance — bilingual manuals + video tutorials provided.

3-Year Warranty + Spares

Core equipment 3-year warranty, electrical 2-year. Spare parts in stock with global express shipment 24h dispatch.

Inputs for line sizing

Send these 3 input sets for an engineering-fit proposal

A useful line proposal starts with your actual output target, cabinet workpieces and fixture plan. Preliminary drawings are enough for the first review; our engineers will flag missing dimensions before quoting.

1. Capacity input

Defines takt time and automation level

  • Units/day and shifts/day
  • SKU mix and batch size
  • Target takt time or annual output
  • Pilot volume and 3-year ramp-up

2. Workpiece input

Defines mould envelope and process recipe

  • Cabinet and door L × W × H
  • Inner/outer skin material and gauge
  • PU wall thickness and target density
  • Temperature class, refrigerant and market standard

3. Fixture input

Defines curing WIP and changeover method

  • Cabinet and door fixture quantities
  • Existing mould/fixture drawings and interfaces
  • Foam cure time and loading method
  • Available floor space, power and compressed air

Accepted files: PDF, STEP, DXF, DWG, photos with dimensions, or a current product specification sheet. Do not have drawings yet? Send overall L × W × H and wall thickness first.

Send the 3 inputs on WhatsApp

Get a Fast Answer From an Engineer

Two ways to reach us — send the 5-field form below, or message a project engineer directly on WhatsApp.

Request a Tailored Quote for This Line